A low quotation, heavier sheet, tighter tolerance, stainless steel label, or approved sample can look reassuring. None proves that a supplier can consistently deliver parts that work in your assembly, survive their intended environment, and arrive when required.
The useful purchasing principle is fitness for purpose: define what the component must do, then obtain evidence that the proposed material and production process can meet that requirement.
This matters across brackets, cabinets, machine guards, electrical enclosures, and fabricated assemblies. A specification can be demanding yet poorly targeted. A quotation can be inexpensive yet incomplete. A sample can pass inspection while leaving production questions unanswered.
The following five myths confuse an individual purchasing indicator with final delivery performance. Published findings and supplier capability figures are identified by source. Cost comparisons and calculations are explicitly illustrative; they are not industry averages.
1. The Lowest Quotation Means the Lowest Total Cost
Total acquisition cost refers to the purchasing expenditure and buyer-borne costs required to obtain accepted parts at the agreed delivery point.
Unit price is one input. It becomes a reliable comparison only after scope, technical requirements, delivery obligations, and responsibility for defects are aligned.
The US Federal Acquisition Regulation distinguishes between a lowest-price, technically acceptable approach and a tradeoff approach. The latter permits a higher-priced offer when its additional benefits justify the price difference and the decision is documented. This is an example of structured purchasing logic, not a rule governing every international buyer. [Acquisition.gov — FAR Subpart 15.1]
Consider a hypothetical order requiring 1,000 accepted parts. Both base quotations include normal delivery, and the additional costs below are assumed to remain with the buyer.
| Cost item | Supplier A | Supplier B |
|---|---|---|
| Unit price | CNY 90 | CNY 100 |
| Base purchase amount | CNY 90,000 | CNY 100,000 |
| Unreimbursed sorting and rework | CNY 8,000 | CNY 1,000 |
| Additional replenishment and expedited freight | CNY 6,000 | CNY 0 |
| Separately attributable delay loss | CNY 12,000 | CNY 0 |
| Total | CNY 116,000 | CNY 101,000 |
Supplier A’s quotation is 10% lower, but its assumed total cost is CNY 15,000 higher. These figures demonstrate a possible outcome; they do not establish that cheaper suppliers generally perform worse. [Illustrative calculation — hypothetical inputs]
The commercial problem often begins before production. One quotation might include deburring, threaded inserts, protective packaging, and inspection records. Another might assume that these requirements will be agreed later. Comparing the totals without resolving those differences rewards missing information.
Prepare a common quotation schedule covering material designation and condition, thickness, drawing revision, quantities, tooling, welding, finishing, inspection, packaging, freight, and applicable taxes. Ask suppliers to identify exclusions and technical deviations explicitly.
For international orders, also specify the named delivery location and which transport activities the quoted amount includes. Separate ordinary freight from emergency freight caused by a quality or schedule problem.
Avoid double counting. If an agreed replacement charge already includes expedited shipment, do not add that shipment again. If the supplier reimburses sorting, only the unrecovered amount belongs in the buyer’s final cost comparison.
Low price remains an opportunity when the supplier has an efficient process and the requirements are clear. Paying more without evidence of better performance is equally weak purchasing. Compare documented outcomes, then use scenario ranges for uncertainties that have not occurred.
Action: Issue one common quotation schedule and compare the cost per accepted delivered part before awarding the order.
2. Thicker Sheet Always Produces a Better Part
Appropriate sheet thickness refers to the thickness needed to satisfy a component’s functional requirements within its manufacturing and assembly constraints.
Adding material may be justified, but thickness is a design choice rather than a general quality ranking. The purchasing question is whether a proposed change improves required performance without creating unacceptable consequences elsewhere.
For unchanged material density and developed sheet area, moving from 1.0 mm to 1.5 mm increases material volume and mass by 50%. That geometric relationship does not mean the finished component price rises by 50%, or that its load capacity improves by the same percentage. [Geometric calculation — constant density and area]
Manufacturing geometry also needs review. Protolabs specifies a minimum flange length of four times material thickness in its own sheet metal guidelines. That is a service-specific design rule, not a universal forming standard. [Protolabs — Sheet Metal Fabrication Design Guidelines]
Using that rule illustratively, a 1.0 mm sheet requires a minimum flange of 4 mm, while a 1.5 mm sheet requires 6 mm. An existing 5 mm flange would therefore need another review after the thickness change. These are calculated design comparisons, not results from a production trial. [Protolabs — Sheet Metal Fabrication Design Guidelines; illustrative calculation]
A buyer who changes thickness while leaving the remaining drawing untouched has changed the manufacturing problem. Bend geometry, developed dimensions, fastener suitability, and assembly clearances should be checked together.
Start with the part’s task. Is it supporting equipment, protecting an operator, locating another component, or simply covering an opening? Specify the relevant load, permitted deformation, installation space, weight limit, and expected service conditions. Engineering can then judge whether the existing thickness is adequate.
For a hypothetical enclosure panel, the concern might be visible deflection rather than failure. A thickness increase could be one option; a revised shape or support arrangement could be another. Treat these as proposals requiring engineering review and functional validation, rather than assuming one solution wins automatically.
The same discipline protects legitimate upgrades. If verification shows that thicker material is needed, procurement should obtain the associated manufacturing review and revised quotation. Cost pressure should not override a documented functional requirement.
Make the thickness specification measurable. State nominal thickness, permitted variation, the applicable material specification, and whether measurements concern the substrate or finished coated part. Otherwise, buyer and supplier may report different measurements while believing they are checking the same requirement.
Action: Require an engineering review of function, forming geometry, fasteners, and fit before approving any thickness change.
3. Tighter Tolerances Always Mean Better Quality
Functional tolerance refers to the permitted dimensional variation that allows a part to perform and assemble as intended.
A tolerance has value when it protects a requirement. Tightening every dimension can make a drawing harder to produce without improving the finished assembly.
Published capability figures illustrate why feature type matters. For material below 0.13 inches thick, Protolabs lists approximately 0.13 mm for hole-to-hole dimensions, 0.38 mm for bend-to-hole dimensions, and 0.76 mm across three or more bends. Buyers should confirm the tolerance convention and applicability for their quotation. These are one supplier’s figures, not universal acceptance limits. [Protolabs — Sheet Metal Fabrication Design Guidelines]
Suppose a drawing requests a deviation allowance of 0.05 mm for each category. Comparing allowance magnitudes gives the following illustrative ratios.
| Feature category | Published allowance magnitude | Requested magnitude | Tightening ratio |
|---|---|---|---|
| Hole to hole | 0.13 mm | 0.05 mm | 2.6 |
| Bend to hole | 0.38 mm | 0.05 mm | 7.6 |
| Across three or more bends | 0.76 mm | 0.05 mm | 15.2 |
The ratios are arithmetic comparisons. They do not predict proportional increases in price, inspection time, or rejection rate. [Protolabs — Sheet Metal Fabrication Design Guidelines; illustrative calculation]
The practical lesson is to separate features by purpose. A locating interface may need close control. A non-mating cover edge may permit more variation. Applying the same requirement to both hides the distinction that manufacturing and inspection teams need.
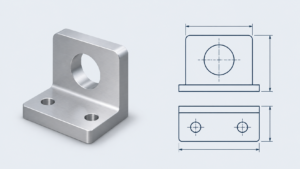
Imagine a bracket that must locate a sensor relative to a mounting surface. The useful review asks which dimensions establish that relationship and how the complete assembly varies. A tight hole diameter alone does not answer whether the sensor reaches the correct position.
Agree on datums, inspection equipment, and measurement condition. A flexible fabricated part measured freely may behave differently when installed. If the drawing requires a defined fixture or restrained condition, describe it so both parties can reproduce the measurement.
Tight tolerances are appropriate when assembly or function demands them. The opportunity lies in applying precision selectively: protect critical interfaces while allowing engineering-approved flexibility elsewhere.
Ask the supplier to identify every requirement outside its normal capability and explain the proposed manufacturing and inspection route. Evaluate any extra cost and lead time against the function being protected.
For recurring production, distinguish conformance from capability. A measured part can pass today without proving that the process will remain predictable. NIST’s statistical terminology links process capability to a stable process; a capability index should therefore be assessed with the underlying process evidence. [NIST — Engineering Statistics Handbook Glossary]
Action: Review tolerances by functional importance and obtain explicit supplier confirmation for every demanding interface.
4. All Stainless Steel Is Rustproof
Corrosion suitability refers to the compatibility between a material, its fabricated condition, and the environment in which it must operate.
“Stainless steel” is an incomplete purchasing specification. A grade designation is more informative, but it still needs service conditions and fabrication requirements before it becomes a defensible material choice.
A field study published by Outokumpu examined stainless steels at six wastewater treatment plants in Sweden and Denmark. Welded AISI 304 experienced localized corrosion at four plants with chloride concentrations above 200 mg/L. AISI 316 was attacked at one plant where chloride exceeded 500 mg/L, alongside elevated electrochemical potential and tightly adherent deposits. No corrosion was found on 2205 in those field exposures. [Outokumpu — MIC on Stainless Steels in Wastewater Treatment Plants]
Those observations disprove a blanket rustproof claim. They do not create universal safe chloride limits, establish a general failure rate, or guarantee that 2205 works in every application. The findings belong to the tested conditions. [Outokumpu — MIC on Stainless Steels in Wastewater Treatment Plants]
For buyers, the main implication is to describe exposure before asking for a material recommendation. “Outdoor use” or “wet environment” leaves too much unanswered. Will the part collect standing water? What cleaning chemicals contact it? What temperatures occur? Are deposits removed regularly?
A hypothetical indoor cabinet in a dry room and a fabricated cover exposed to contaminated wash water should not automatically share a specification merely because both are called enclosures. Their material reviews need different information.
Provide the supplier or materials engineer with the medium, chloride information where relevant, temperature range, pH, cleaning routine, and likely crevices or deposits. Where the information is uncertain, identify the uncertainty instead of silently assuming benign conditions.
Also define the fabricated surface condition. State the required treatment of weld discoloration and whether pickling, passivation, or another specified treatment is required. The process should be selected for the actual material and application.
This creates opportunities as well as controls. A well-defined environment may support an economical material choice. Conversely, demanding exposure may justify a different grade, redesigned detail, or revised maintenance plan. Neither automatic upgrading nor automatic cost reduction is a substitute for evaluation.
Require the material designation, applicable specification, condition, and agreed traceability documents in the purchase order. Keep material identity separate from evidence of environmental suitability: knowing what was supplied does not, by itself, prove that it will survive the intended service.
Action: Approve stainless steel against a written exposure specification and fabricated-condition requirements rather than a generic rustproof claim.
5. An Approved Sample Proves Stable Mass Production
Production readiness refers to demonstrated ability to repeatedly meet agreed requirements under the intended manufacturing conditions.
An approved sample establishes something narrower: the inspected sample met the characteristics actually checked. It does not automatically validate every feature, future batch, or changed production route.
Sampling uncertainty alone should make buyers cautious. NIST explains that normal-approximation confidence limits can be inadequate when sample sizes or failure counts are small, and describes exact binomial methods as an alternative. [NIST — Exact Binomial Confidence Limits]
For independently sampled parts from one stable process, with zero observed nonconforming units, the one-sided 95% exact upper confidence limit for the nonconforming proportion is:\[ p_U = 1 – 0.05^{1/n} \]
Here, \(n\) is the sample size. Applying that model gives:
| Randomly inspected parts, all conforming | One-sided 95% upper confidence limit |
|---|---|
| 30 | Approximately 9.5% |
| 100 | Approximately 3.0% |
| 300 | Approximately 1.0% |
These are calculated statistical limits, not measured supplier defect rates. They show how much uncertainty can remain after observing no defects. The confidence statement concerns the method’s long-run coverage; it does not assign a probability to a fixed unknown defect rate. [NIST — Exact Binomial Confidence Limits; calculation under stated assumptions]
When I work through this example, I use 30 accepted pieces as the starting point and substitute \(n = 30\) into the equation. The result is approximately 9.5%, even though the observed nonconforming count is zero. This is a desk calculation using the stated model, not a factory experiment or a report of my own production experience. It demonstrates why “every sample passed” is a limited claim. [Illustrative calculation using the NIST exact-binomial method]
The assumptions matter. Hand-selected samples, specially repaired pieces, or samples made on a different route do not provide the same basis for inference. Neither does a batch containing important changes that the sampling model ignores.
Separate sample approval from production approval. Record the intended equipment, tooling, material, program revision, inspection method, and relevant production conditions. Ask whether the trial actually represents the process that will supply the order.
Request raw measurements for critical features rather than accepting only a pass stamp. The records should identify what was measured, how it was measured, and which parts or production conditions the results represent.
Scale verification to the consequences of failure. A low-risk cosmetic component and an interface essential to assembly may need different controls. Avoid turning one sample size or capability threshold into a purchasing rule for every product.
Finally, agree how changes are controlled. Define which material, tooling, process, or production-location changes require notification or renewed approval. Sample approval becomes more useful when it establishes a controlled reference for later deliveries.
Action: Approve the sample and production process separately, using representative evidence and a written change-control agreement.
Foire aux questions
A: When quotations cover comparable requirements and credible evidence supports the necessary quality and delivery performance. Low price can reflect efficiency. Confirm exclusions, acceptance requirements, packaging, delivery scope, and responsibilities before treating the price difference as a saving.
A: Only after engineering review establishes a functional need. Thickness changes should trigger checks of geometry, weight, hardware, and fit. Ask for a validated comparison of the proposed options rather than changing thickness independently of the drawing.
A: Dimensions governing function, locating relationships, and assembly deserve focused review. Set their requirements through engineering analysis and confirm the manufacturing and measurement methods. Other dimensions should have tolerances appropriate to their purpose rather than inheriting unnecessary precision.
A: No grade designation provides an unconditional service guarantee. Describe the exposure and fabricated condition, including cleaning and deposits. Have the proposed grade and treatment reviewed against those conditions, especially where corrosion would have serious consequences.
A: A larger representative sample can reduce sampling uncertainty under an appropriate model. It cannot compensate for selected samples, unverified measurement, or a different production process. Combine sampling with process evidence, agreed acceptance rules, and control of subsequent changes.
A: Obtain the agreed drawing revision, material specification, supplier deviations, delivery scope, acceptance plan, critical-feature evidence, and change-notification requirements. Match the depth of review to the application’s consequences and uncertainty. Resolve open technical questions before treating sample acceptance as authorization for routine production.