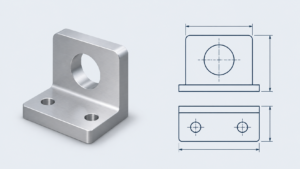
A sheet metal part can pass an inspection report and still fail at assembly. The hole diameters may be acceptable, the outside dimensions may match, and the material certificate may be correct. Yet the bracket needs forcing into position, the connector misses its opening, or the enclosure rocks against its mounting surface.
For buyers, the useful question is whether the drawing controls the relationships that make the part work. Tightening every dimension rarely answers that question. It can increase manufacturing and inspection work while leaving the actual assembly risk untouched.
A stronger procurement specification connects functional requirements, drawing interpretation, manufacturing condition, and acceptance evidence. This guide explains how to build that connection without turning every ordinary flange into a precision machining project.
The numerical assembly examples below are illustrative calculations, not published manufacturing capability limits. Standards status was checked against the issuing organizations’ public catalogs on November 1, 2026.
1. General Tolerances: Choose the Right Standard and Lock the Edition
General tolerances refer to default permissible variations applied to eligible dimensions or features that do not carry individual tolerance requirements.
They keep drawings readable. They also create problems when a familiar title-block note becomes a substitute for technical review.
ISO 2768-1:1989 addresses general tolerances for linear and angular dimensions without individual indications, using four classes: f, m, c, and v. Its scope includes workpieces formed from sheet metal. The ISO catalog still identifies this edition as published while showing its intended replacement, ISO 2768, as under publication. Buyers should therefore specify the agreed edition rather than assume an unqualified reference always means the same document. [ISO 2768-1; ISO 2768 Revision Project]
That distinction matters when drawings circulate between a design office, purchasing team, overseas factory, and independent inspector. Each party needs the same requirements at quotation and acceptance.
The familiar note “ISO 2768-mK” combines different controls. The m identifies a general dimensional tolerance class under Part 1; K belongs to the former general geometrical tolerance system under Part 2. ISO lists ISO 2768-2:1989 as withdrawn and identifies ISO 22081:2021 as its successor. [ISO 2768-2]
This does not justify silently rewriting a legacy purchase specification. An approved drawing may deliberately retain an older edition. Changing that basis requires a controlled engineering decision and agreement about the affected requirements.
ISO 22081:2021 establishes rules for defining and interpreting general geometrical and general size specifications. It was reviewed and confirmed in 2026. It is not simply the old K class with a new document number; its application requires the actual specification, relevant values, scope, and applicable datum references to be established. [ISO 22081]
Other standards perform different jobs:
| Reference | Main procurement role | What the reference alone does not establish |
|---|---|---|
| ISO 2768-1 | General linear and angular dimensional tolerances | Every functional geometrical relationship |
| ISO 22081 | Rules for general geometrical and size specifications | A ready-made replacement for a legacy K-class note |
| ISO 1101 | Language and interpretation of geometrical specifications | A complete procurement inspection package |
| ASME Y14.5 | Dimensioning and GD&T rules within the ASME system | Numerical tolerances for every unspecified dimension |
ISO 1101:2017 covers geometrical specification language, including form, orientation, location, and run-out. ASME lists Y14.5-2018 (R2024), with R2024 indicating reaffirmation of the edition. These references help communicate requirements; the drawing still needs the requirements themselves. [ISO 1101; ASME Y14.5]
The commercial opportunity is clearer quotations. When suppliers price the same technical baseline, differences in tooling, inspection, and manufacturing assumptions become easier to identify. A lower price is meaningful only when the quoted acceptance conditions are comparable.
Raccomandazione operativa: Before releasing an RFQ, record the governing tolerancing system, edition, applicable general tolerance class or specification, and the agreed precedence of conflicting technical documents.
2. Functional Dimensions and Datums: Control the Relationships That Make Parts Assemble
Functional dimensioning refers to specifying dimensions and geometrical relationships according to how a part locates, connects, seals, or operates in its intended assembly.
Start with the assembly interface. Identify which surface seats against the frame, which feature locates the part sideways, and which feature prevents the remaining movement. Then define the drawing controls around those relationships.
A convenient cut edge is not automatically a useful datum feature. If the product locates through mounting holes but inspection aligns everything to an unrelated outside edge, the report can answer the wrong question.
Consider a bracket fastened to a rigid base with fixed threaded holes. Assume a maximum effective screw diameter of 6.0 mm and a minimum clearance-hole diameter of 6.6 mm. The ideal radial clearance is:
Available center offset = (6.6 − 6.0) / 2 = 0.30 mm. [Illustrative Engineering Calculation]
That figure is only a starting assembly budget. It excludes mating-part hole-location error, hole-axis tilt, coating, hole form, and the interaction between several fasteners. It must not be copied directly into a position tolerance without analyzing the complete interface.
The example exposes a common purchasing mistake: asking for extremely consistent hole diameters while leaving the hole pattern inadequately located. The supplier can meet the diameter requirement and still produce parts that do not fit.
The reverse mistake is also expensive. If the assembly has sufficient clearance or an intentional adjustment slot, forcing unnecessarily tight locations on every nearby feature may add work without improving function.
A practical drawing review separates characteristics by their role:
| Characteristic | Requirement to evaluate |
|---|---|
| Ordinary nonmating edge | Suitable general dimensional tolerance |
| Fastener clearance hole | Hole size and its functional location |
| Locating hole | Size, geometry, and relationship to assembly datums |
| Mounting surface | Required form and, where relevant, orientation |
| Connector opening | Final position or profile relative to assembly references |
| Cosmetic surface | Defined appearance criteria and inspection conditions |
This is an engineering review framework, not a tolerance table supplied by a standard. Actual values require design justification and supplier feasibility review.
For a mounting bracket, the seating surface might establish datum A, a functional side feature datum B, and an end-locating feature datum C. The exact scheme depends on the assembly. Simply labeling three convenient surfaces A, B, and C does not prove the scheme reproduces the installed condition.
Ask the supplier to explain how its fixture and measurement alignment establish the specified references. An unrestricted best-fit alignment may distribute deviations across the model while concealing the relationship that matters to installation. The inspection program must evaluate the drawing’s requirement.
There is also a design opportunity here. A revised datum scheme, controlled floating interface, or correctly placed slot may improve interchangeability more effectively than tighter cutting tolerances. Such changes require engineering approval, but they can reduce assembly effort and unnecessary manufacturing constraints together.
Raccomandazione operativa: Review each mating interface with design and inspection personnel, then assign explicit size and geometrical controls only after confirming the actual assembly location scheme.
3. Formed-Part Condition: Specify What Is Measured and When
Inspection condition refers to the manufacturing stage, support arrangement, and restraint state in which a specified characteristic is evaluated.
Sheet metal is sensitive to this definition. A flexible panel resting on a table, supported at designated points, or fastened to an assembly fixture can produce different measurement results. All three setups may be repeatable while representing different conditions.
The procurement drawing should identify whether the requirement applies after forming, welding, hardware insertion, or finitura superficiale. A flat-pattern measurement cannot demonstrate every requirement of the finished assembly.
A long flange illustrates the problem. For an idealized 100 mm flange with a 0.5° angular deviation, the lateral displacement at its end is approximately:
End displacement = 100 × tan(0.5°) = 0.873 mm. [Illustrative Engineering Calculation]
Precise cutting of the original blank does not remove that angular contribution. If a connector sits near the flange tip, its final position can be more important than the original blank length.
In a desk calculation for this guide, I checked the same 100 mm flange at angular deviations of 0.1°, 0.2°, and 0.5°. The calculated tip offsets were approximately 0.175 mm, 0.349 mm, and 0.873 mm respectively. This was a numerical observation, not a factory measurement trial. It showed why I would review the formed connector interface before requesting tighter flat-pattern cutting: the angular contribution can dominate the interface error budget. [Calculation Performed for This Article]
The useful response depends on function. A rigid connector interface may need a controlled final location. A floating connection may accommodate variation. A cosmetic return flange may require a different acceptance criterion entirely.
Coating creates another condition question. Where finish affects clearance, contact, or seating, specify whether acceptance applies before or after coating. If a contact surface must remain uncoated, identify the masking area rather than rely on a verbal instruction.
For flexible parts, a controlled inspection sketch can communicate the setup more efficiently than a long note. It can identify supports, locating features, clamps, tightening sequence, and any specified force or torque. It should distinguish characteristics inspected under restraint from those required in the free state.
The fixture also deserves review. It should reproduce the intended condition without unintentionally forcing an unacceptable part into an apparently acceptable shape. Equally, demanding free-state geometry everywhere may impose unnecessary constraints on a panel designed to function when installed.
The opportunity is agreement before production. Buyer and supplier can evaluate the same physical condition, reducing repeated measurements and arguments about whose report is correct. The specification should describe the required product behavior while leaving reasonable freedom in the manufacturing route.
Raccomandazione operativa: Add a controlled inspection-condition note or sketch covering finished state, supports, restraints, and coating treatment for every flexible or assembly-sensitive feature.
4. First-Article Evidence and Measurement Reports: Make Results Reproducible
First-article inspection refers to a documented evaluation of initial production parts against the specified requirements under identified manufacturing conditions.
A useful first-article package establishes more than sample approval. It connects the physical samples to the drawing revision, production route, inspection method, and any authorized deviations.
For procurement, the strongest records let another competent reviewer follow each requirement to its evidence. A report containing only “OK” removes information that may later explain assembly problems or process changes.
Request a ballooned drawing or equivalent characteristic index, with individual measured results linked to identifiable samples. Include applicable drawing notes and general tolerances in the review. Material, coating, inserted hardware, and other specified requirements need appropriate evidence even when they are not ordinary dimensions.
The following is a suggested purchasing checklist, not a universal first-article form mandated by the tolerancing standards:
| Record group | Useful contents |
|---|---|
| Product identity | Part number, drawing revision, order reference, sample identity |
| Production history | Material batch, relevant tooling, process route, subcontract operations |
| Requirement traceability | Characteristic number, specification, units, datum references |
| Actual results | Individual values, status, exceptions, retest results |
| Measurement setup | Equipment, program revision, fixture, alignment, restraint condition |
| Approval history | Inspector, reviewer, date, authorized deviation reference |
This structure helps distinguish a product problem from an interpretation or measurement problem. A change in fixture alignment, for example, may explain differences between reports even when the manufacturing route is unchanged.
Measurement traceability also needs careful language. NIST describes it as a property of a measurement result supported by a documented, unbroken calibration chain, with contributions to measurement uncertainty. An instrument’s calibration status alone does not describe the uncertainty of every task performed with it. [NIST Metrological Traceability]
For thin sheet metal, relevant influences can include support, clamping, temperature, probing, sampling density, and data evaluation. Their importance depends on the feature and the measurement method. A caliper display with additional decimal places does not establish that the complete measurement is suitable for a demanding acceptance decision.
First-article approval should also identify the conditions it covers. Procurement teams can define review triggers for drawing changes, tooling changes, significant process changes, or relocation. The extent of reinspection should match the characteristics potentially affected.
There is a cost tradeoff. Requiring elaborate reports for every cosmetic dimension can consume resources better spent on functional interfaces. Conversely, accepting a generic inspection certificate for a complex formed assembly can hide the evidence needed to establish fit.
A proportionate package puts detailed measurements and setup records where failures matter, while using appropriate documentation for routine requirements. It also preserves concessions explicitly: a sample accepted with a deviation should not quietly redefine the drawing for future deliveries.
Raccomandazione operativa: Approve the first-article report format and measurement setup before production, including characteristic indexing, individual sample results, revision traceability, and deviation handling.
5. Sampling and Acceptance Decisions: Agree the Rules Before Shipment
Acceptance planning refers to defining how inspection results, sampling risk, and measurement uncertainty determine the disposition of parts or production lots.
A first article and a shipment sample answer different questions. The former evaluates identified initial parts and conditions. The latter supports a decision about a defined production lot.
NIST describes a single sampling plan as a random sample from a lot followed by a disposition decision based on the observed nonconforming items. Its explanation identifies sample size and the acceptance threshold as essential plan elements. A note containing only “AQL 1.0” therefore leaves important instructions missing. [NIST Acceptance Sampling Handbook]
A purchasing plan should define the lot, relevant defect categories, sampling method, sample size, acceptance and rejection numbers, and disposition rules. When a formal sampling standard is used, identify the edition and applicable inspection levels and switching rules.
AQL is not a guarantee that every delivered lot stays below the stated percentage. Likewise, finding no failures in a sample does not establish a defect-free shipment. The plan manages decision risk; it does not inspect unmeasured parts. [NIST Acceptance Sampling Handbook]
Severity matters. A cosmetic scratch, a misplaced mounting hole, and a failure affecting safety should not automatically share the same control strategy. Additional process controls, functional checks, or complete inspection may be justified for particular characteristics, subject to the consequences and the effectiveness of the method.
Measurement uncertainty creates a separate decision issue near specification limits. NIST’s quality information framework discussion connects measurement results, uncertainty, tolerances, and conformity assessment. Buyers should establish the decision rule before a borderline result appears. [NISTIR 8127]
Consider an illustrative requirement of 10.00 ± 0.10 mm. The permissible interval is 9.90–10.10 mm. A measured result of 10.09 mm with expanded uncertainty U = 0.03 mm gives an uncertainty interval of 10.06–10.12 mm. [Illustrative Engineering Calculation]
Under an agreed conservative rule requiring that interval to remain within specification, this result does not demonstrate conformity. It also does not, by itself, demonstrate nonconformity. The next step follows the agreed procedure, such as improved measurement, technical review, or controlled disposition. [NISTIR 8127]
This distinction prevents an avoidable argument: the supplier points to the displayed value, while the buyer introduces a stricter uncertainty rule after shipment. Both sides need to understand the same acceptance basis when quoting and planning inspection.
Define rejected-lot handling as well. Specify identification, segregation, sorting or rework, and the evidence required for resubmission. Randomly selecting another sample until a lot passes undermines the original decision process.
The practical opportunity is predictable release. Clear rules allow inspection effort to follow functional risk, give suppliers a workable target, and keep commercial discussions tied to evidence.
Raccomandazione operativa: Attach a controlled acceptance plan to the order covering lot sampling, characteristic severity, uncertainty decision rules, borderline results, and rejected-lot resubmission.
Domande frequenti
A: It is an incomplete procurement basis for many parts. It combines dimensional and legacy geometrical classes without explaining critical interfaces, finished condition, or inspection. Identify the intended editions and develop any migration through controlled engineering review.
A: No. It establishes a different framework for general specifications. The engineering revision needs to define the actual requirements and their application rather than substitute a document number.
A: No. It supplies dimensioning and GD&T rules. Numerical dimensions, applicable tolerances, and general requirements still need to be specified in the technical documentation.
A: Set tolerances from function and verify feasibility. Tight control is valuable where it protects fit, sealing, or interchangeability. Elsewhere, excessive constraints can add tooling, correction, inspection, and rejection costs without improving the assembly.
A: No. It provides evidence for the evaluated samples and manufacturing conditions. Ongoing production requires appropriate controls, change management, and an agreed lot acceptance process. Keep first-article approval and shipment acceptance as separate decisions.
A: Apply the agreed decision rule and relevant uncertainty. If conformity cannot be demonstrated under that rule, follow the prescribed review or remeasurement process. Do not invent a stricter acceptance rule after the result is known.